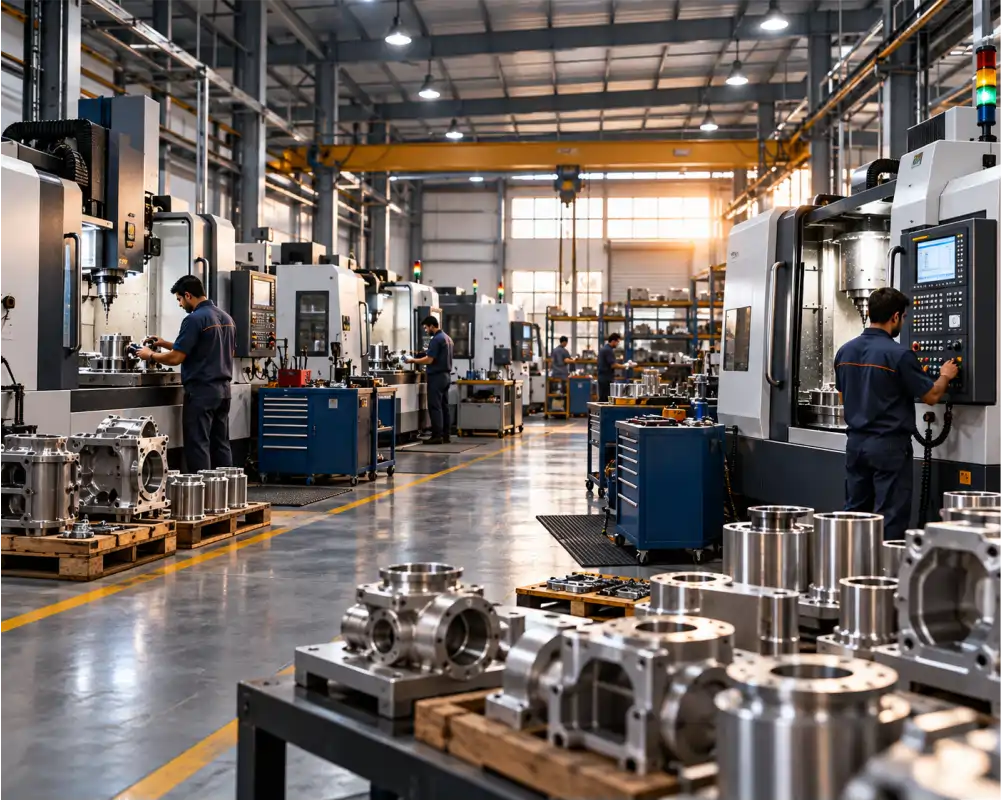
Investment castings arrive close to net shape, so only critical faces need machining. Having that machining in the same works removes a supplier from your chain, shortens lead time and keeps responsibility for the finished dimension in one place.
Supply condition can be raw, finished or assembled, entirely as per your demand. Fixtures and gauges are designed and built in our own tool room so that repeat batches load and check the same way every time.
Discuss MachiningTurning centres for flanged bodies, bushes, sleeves and rotationally symmetric components, holding concentricity across multiple diameters in one setting.
Milling of faces, pockets, slots and bolt patterns on valve bodies, pump casings and brackets, with fixtures built in our own tool room.
Through and blind holes, counterbores and threaded ports produced to gauge, including NPT, BSP and metric threads.
Surface and cylindrical grinding for seat faces and sealing surfaces where flatness and finish are critical to leak tightness.
Sub-assembly of machined castings with bought-out items, pressure testing where required, and packing as a ready-to-fit unit.
First-off approval, patrol inspection and final gauging against the drawing, with results recorded for each batch.
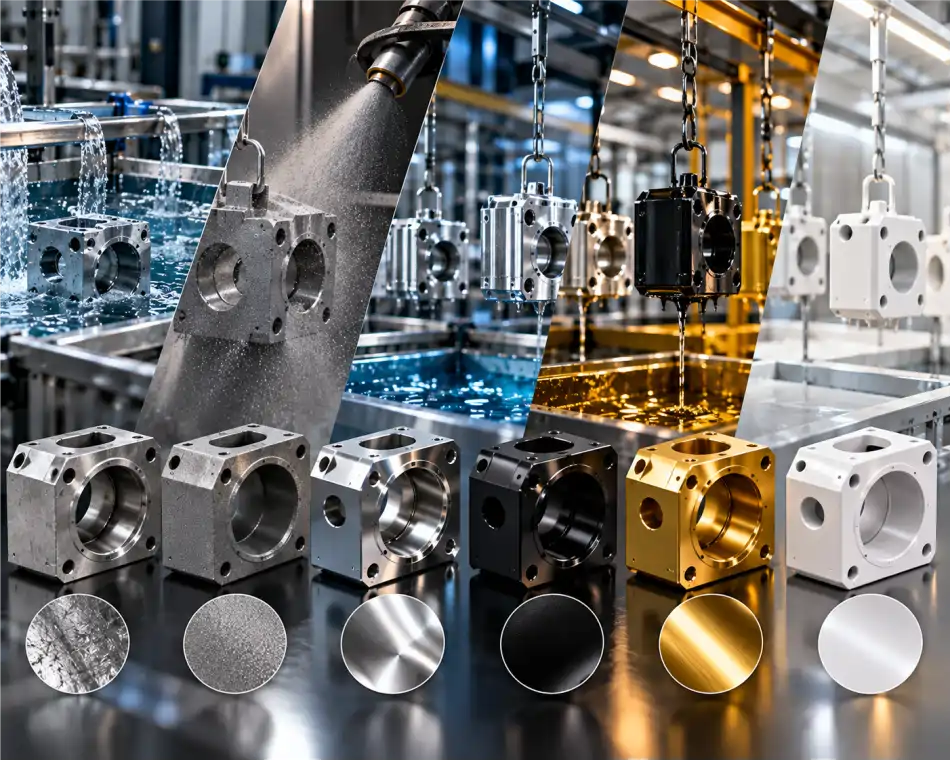
Machined components move straight into surface treatment so they leave the works ready to fit, protected for transit and matched to the appearance your end market expects.
A complete lost wax line from wax room to despatch, rated at 950 MT per annum.
ViewIn-house die design and manufacture, plus lifetime storage and maintenance of your tooling.
ViewSimulation, design support and process engineering behind every component we cast.
ViewShare the finished part drawing along with the casting drawing. We will quote cast, machined and assembled options so you can compare the true landed cost.
Request a Quotation